
Capacity, Supply & Constraint Planning
A festive-season forecast jumps overnight, but the factory cannot add a second paint booth, the supplier cannot ship more chips, and the warehouse has only two loading docks. The real planning question is no longer “How much can we sell?” - it is “What can the system actually deliver, and where will it break first?”
- Capacity planning decides how much output a process, plant, workforce or supplier network can realistically produce in a period.
- Supply planning converts demand into a feasible supply plan using inventory, production, procurement and distribution choices.
- Constraint planning focuses on the bottleneck - the resource that limits total system output.
- The goal is not maximum utilization everywhere. The goal is profitable service at the constraint-aware optimum.
- Use a simple sequence: demand signal - available capacity - constraint check - supply allocation - exception management.
- Core metrics: utilization, capacity cushion, service level, backlog, throughput and schedule adherence.
- Common interview trap: treating every resource equally instead of identifying the binding constraint.
Big Picture: Planning Is a Feasibility Filter, Not a Spreadsheet Exercise
Demand planning tells you what the market may want. Capacity, supply and constraint planning tell you what the business can promise without breaking service, cost or cash. If you have not revised demand fundamentals, start with why demand planning decides everything downstream, because capacity planning is the reality check placed on top of that demand signal.
Core Explanation: The Three Layers You Must Not Confuse
Think of this topic as three stacked questions. Capacity asks, “How much can we make or move?” Supply asks, “How will we fulfill demand?” Constraint planning asks, “Which limiting factor decides the whole plan?”
1. Capacity Planning
Capacity planning is deciding the resources required to meet expected demand over a chosen time horizon. Resources may include machines, labor hours, supplier output, storage space, transport vehicles, cash limits or even management bandwidth.
Capacity has three useful forms:
- Design capacity: the theoretical maximum under ideal conditions.
- Effective capacity: the realistic maximum after maintenance, changeovers, absenteeism, mix complexity and quality losses.
- Available capacity: what is actually available in the planning window after current commitments.
2. Supply Planning
Supply planning translates demand into production, procurement, inventory and distribution decisions. It answers: make now or later, buy more or ration, allocate to which customer or region, and when to expedite.
A good supply plan is not simply “meet all demand.” It balances service level, cost, inventory, lead time and capacity feasibility. This is where the monthly Sales and Operations Planning cycle becomes important, because demand, supply, finance and leadership must agree on one feasible plan.
3. Constraint Planning
Constraint planning identifies the resource that limits total output and plans the system around it. A non-bottleneck improvement may look efficient locally but create no additional customer service if the true bottleneck remains unchanged.
“I would first separate demand from feasible supply, then identify the binding constraint. The plan should protect the bottleneck, not optimize every department independently.”
Definitions You Can Say in One Breath
- Capacity: The maximum output a process or resource can deliver in a defined period under specified conditions.
- Supply plan: A time-phased plan for meeting demand using inventory, production, procurement and distribution decisions.
- Constraint: The limiting factor that prevents a system from achieving higher throughput or service.
- Bottleneck: The resource with insufficient capacity relative to demand, restricting the output of the whole process.
The Constraint Planning Logic: Protect the Bottleneck
The central idea is simple: the system’s output is governed by its tightest resource. If the paint shop can handle 800 units per day but assembly can handle 1,000, the system cannot ship 1,000 finished units unless paint capacity is increased, outsourced, rescheduled or the product mix changes.
Constraint planning usually follows five moves:
Key Metrics: How to Measure Whether the Plan Is Working
In interviews, metrics separate a polished answer from a vague one. Use 4-6 measures, state the formula, and explain what “good” depends on.
Worked Example: Finding the Bottleneck in 3 Minutes
A company plans to produce 900 units next week. The product passes through three resources:
Answer: Painting is the bottleneck. The feasible weekly output is 750 units unless the company adds painting capacity, outsources painting, reduces paint-intensive product mix, uses finished goods inventory or shifts some demand to the next period.
The important interview point: increasing assembly capacity from 950 to 1,100 does not improve shipments. The constraint is painting, so management attention must go there first.
Capacity Responses: What a Manager Can Actually Do
Once you identify the gap, do not stop at “increase capacity.” Interviewers expect trade-offs. Use this menu:
This is also where the bullwhip effect matters: if upstream capacity decisions are based on noisy, inflated demand signals, the business may overbuild capacity and still stock the wrong items.
Case Study: Maruti Suzuki and Semiconductor-Constrained Production
Maruti Suzuki had to manage vehicle production through semiconductor supply constraints, showing why the binding constraint can sit outside the factory.
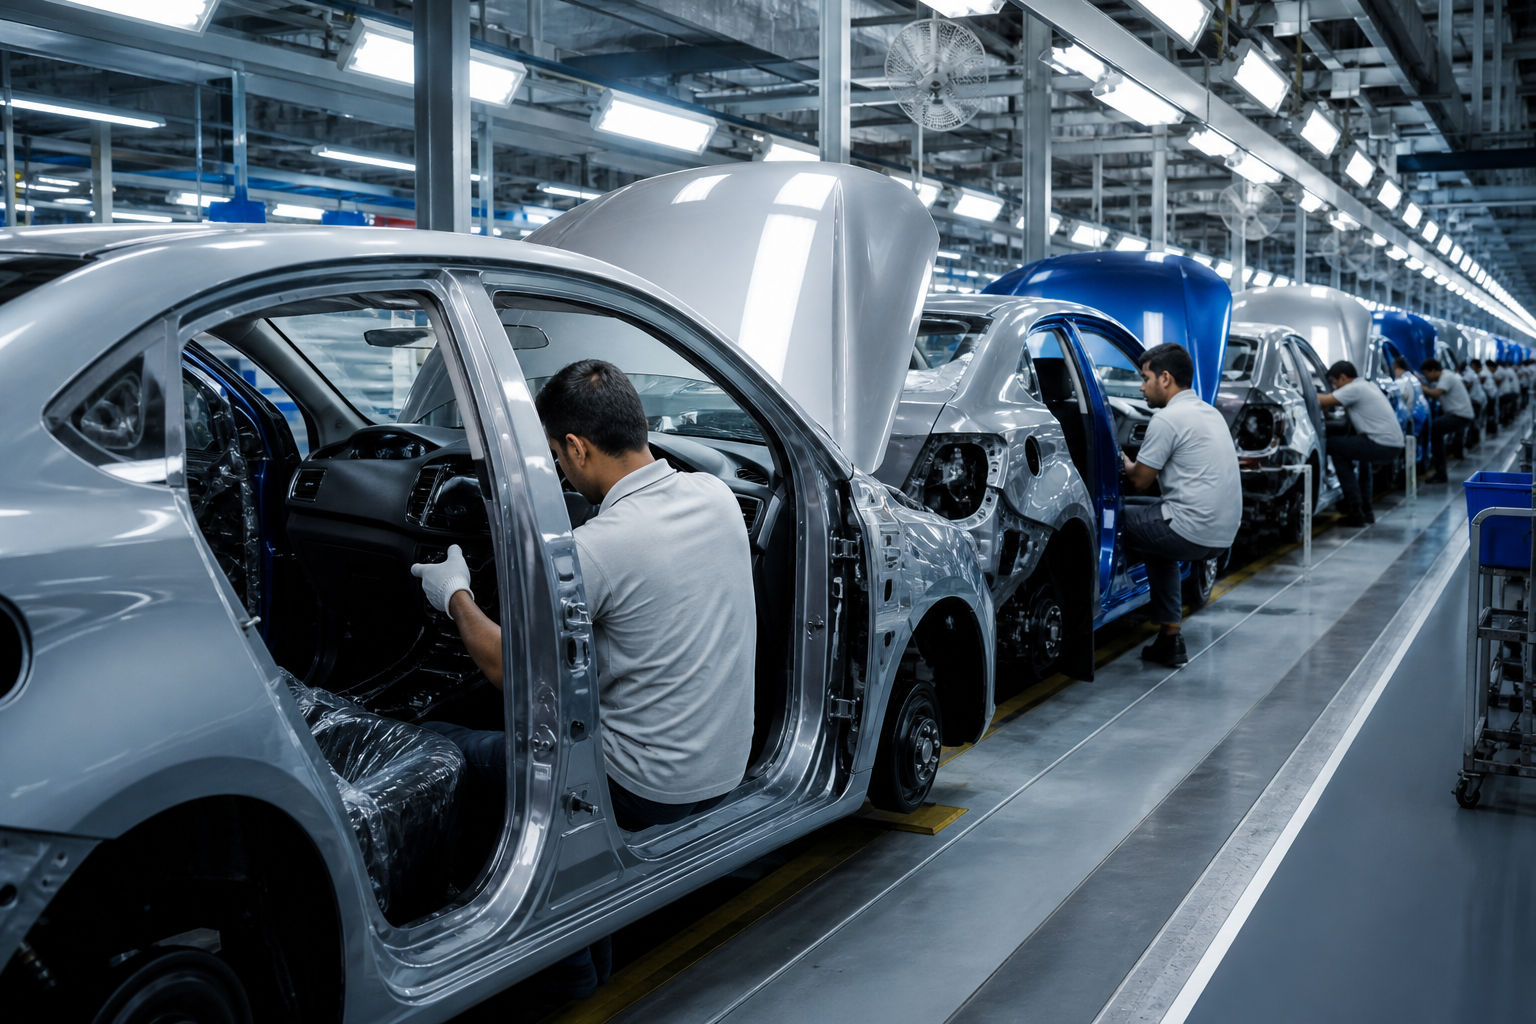
Situation: During the global semiconductor shortage, automakers faced a constraint that was not simply labor, assembly capacity or showroom demand. A vehicle could not be completed if critical electronic components were unavailable. Maruti Suzuki discussed the impact of semiconductor availability on production in its public investor communications and annual reports (Maruti Suzuki annual reports).
The move: The planning challenge was to convert demand into feasible supply under a component bottleneck. That meant prioritizing production based on component availability, coordinating closely with suppliers, adjusting schedules, and managing dealer/customer expectations. The primary driver was semiconductor allocation. Supporting drivers included product-mix decisions, supplier coordination, production rescheduling, and communication across sales and operations.
Outcome / lesson: The case proves that capacity is not only inside the plant. In a complex supply chain, the true constraint may be a tier-2 or tier-3 component. A strong planner asks, “Which scarce input controls output?” before promising volume.
How AI Changes Capacity, Supply & Constraint Planning
AI is making planning faster, but not magically unconstrained. The biggest shift is that planners can now detect constraints earlier and simulate more options before committing the plan.
- ML-based demand sensing: AI can absorb point-of-sale trends, search signals, weather, promotions and regional demand shifts faster than manual planning. This improves the input to capacity planning, especially when paired with demand sensing signals and point-of-sale data.
- Constraint-aware optimization: Advanced planning systems can run feasible supply scenarios across plants, suppliers, inventory and logistics. The planner’s role shifts from building spreadsheets to choosing the best trade-off among service, cost and risk.
- Early-warning exception management: AI can flag likely supplier delays, capacity overloads, abnormal backlogs and schedule adherence risks before the monthly review meeting.
Use NotebookLM or ChatGPT with a company annual report and ask: “Identify the company’s major supply constraints, capacity expansion signals, inventory risks and likely interview questions on its operating plan.” Then verify every factual claim from the report before using it.
Interview Relevance
“Demand for a product is forecast at 1 lakh units next month, but the plant can produce only 80,000 units and a key supplier can support only 70,000 units. How would you build the supply plan?”
Always say what you would not do: “I would not plan 1 lakh units just because demand exists; I would first resolve or allocate around the 70,000-unit supplier constraint.”
Common Mistake
The biggest mistake is treating capacity planning as “increase all resources.” That wastes money because non-bottleneck capacity does not increase system output. The one-line fix: find the binding constraint first, then plan every response around it.