
Overall Equipment Effectiveness Explained and Calculated
A machine running all day can still be a bad operation. The common misconception is that “high utilization” means “high productivity” - but a line can be busy producing slowly, stopping often, or making rejects.
Overall Equipment Effectiveness fixes that blind spot. It asks one ruthless question: of the time we planned to produce, how much became good output at the intended speed?
- OEE = Availability × Performance × Quality.
- Availability captures downtime loss: did the equipment run when it was scheduled to run?
- Performance captures speed loss: did it run as fast as the ideal cycle time?
- Quality captures defect loss: how much output was good the first time?
- Calculate OEE using planned production time, not total calendar time.
- A lower OEE is not always bad - it may reflect high product variety, planned maintenance, or deliberate flexibility.
- In interviews, never stop at the percentage. Split the loss and recommend the first improvement lever.
Big Picture: OEE Is a Loss-Diagnosis Tool, Not a Vanity Score
OEE works because it separates one big performance problem into three operational losses. If output is low, the cause could be that the machine was unavailable, running below speed, or producing bad units. Each cause needs a different managerial response.
Core Explanation: The Three Parts of OEE
Overall Equipment Effectiveness measures how effectively a machine, line, or asset converts planned production time into good output at standard speed.
The clean formula is:
OEE = Availability × Performance × Quality
1. Availability - Did the asset run when it was supposed to?
Availability = Run Time ÷ Planned Production Time
Availability falls when the line is stopped during scheduled production. Causes include breakdowns, tooling delays, material shortages, waiting for quality clearance, or unplanned changeover overruns.
2. Performance - Did the asset run at the intended speed?
Performance = Ideal Cycle Time × Total Count ÷ Run Time
Performance falls when equipment is technically running but slower than the standard rate. Causes include minor stops, idling, inexperienced operators, speed restrictions, micro-jams, or poor line balancing and workstation design.
3. Quality - Was the output good the first time?
Quality = Good Count ÷ Total Count
Quality falls when units require rework or are scrapped. Causes include process drift, wrong settings, raw material issues, operator error, or weak in-process checks.
Worked Example: Calculate OEE in Four Lines
A packaging line runs one 8-hour shift. Planned break time is 30 minutes. During the shift, the line has 60 minutes of unplanned downtime. The ideal cycle time is 0.5 minute per unit. It produces 700 total units, of which 665 are good.
The answer is not “73.8% is good or bad” by itself. The useful insight is that the largest loss is the combined effect of downtime and speed loss, so the first diagnostic should investigate stoppages and minor-speed losses before blaming quality.
Definitions You Must Say Cleanly
- OEE: The percentage of planned production time converted into good output at ideal speed.
- Availability: The share of planned production time during which the equipment actually runs.
- Performance: The share of run time converted into output at the ideal cycle rate.
- Quality: The share of total output that is good without scrap or rework.
- Planned production time: Scheduled production time excluding planned stops such as breaks, maintenance windows, or no-demand periods.
OEE Metrics: What to Track and What “Good” Looks Like
Use these as interview heuristics, not universal benchmarks. A pharma filling line, a paint batch plant, and a CNC job shop should not be judged by the same number without context.
The OEE Improvement Loop
OEE becomes powerful when it is treated as a recurring improvement loop. The best teams do not “report OEE”; they use it to find the biggest loss, fix the root cause, standardise the fix, and keep watching for drift.
Case Study - Asian Paints: Applying OEE to a High-Mix Indian Plant
Asian Paints is a useful Indian case because paint manufacturing combines high SKU variety, batch processing, filling lines, and service-level pressure - exactly the conditions where OEE must be interpreted carefully.
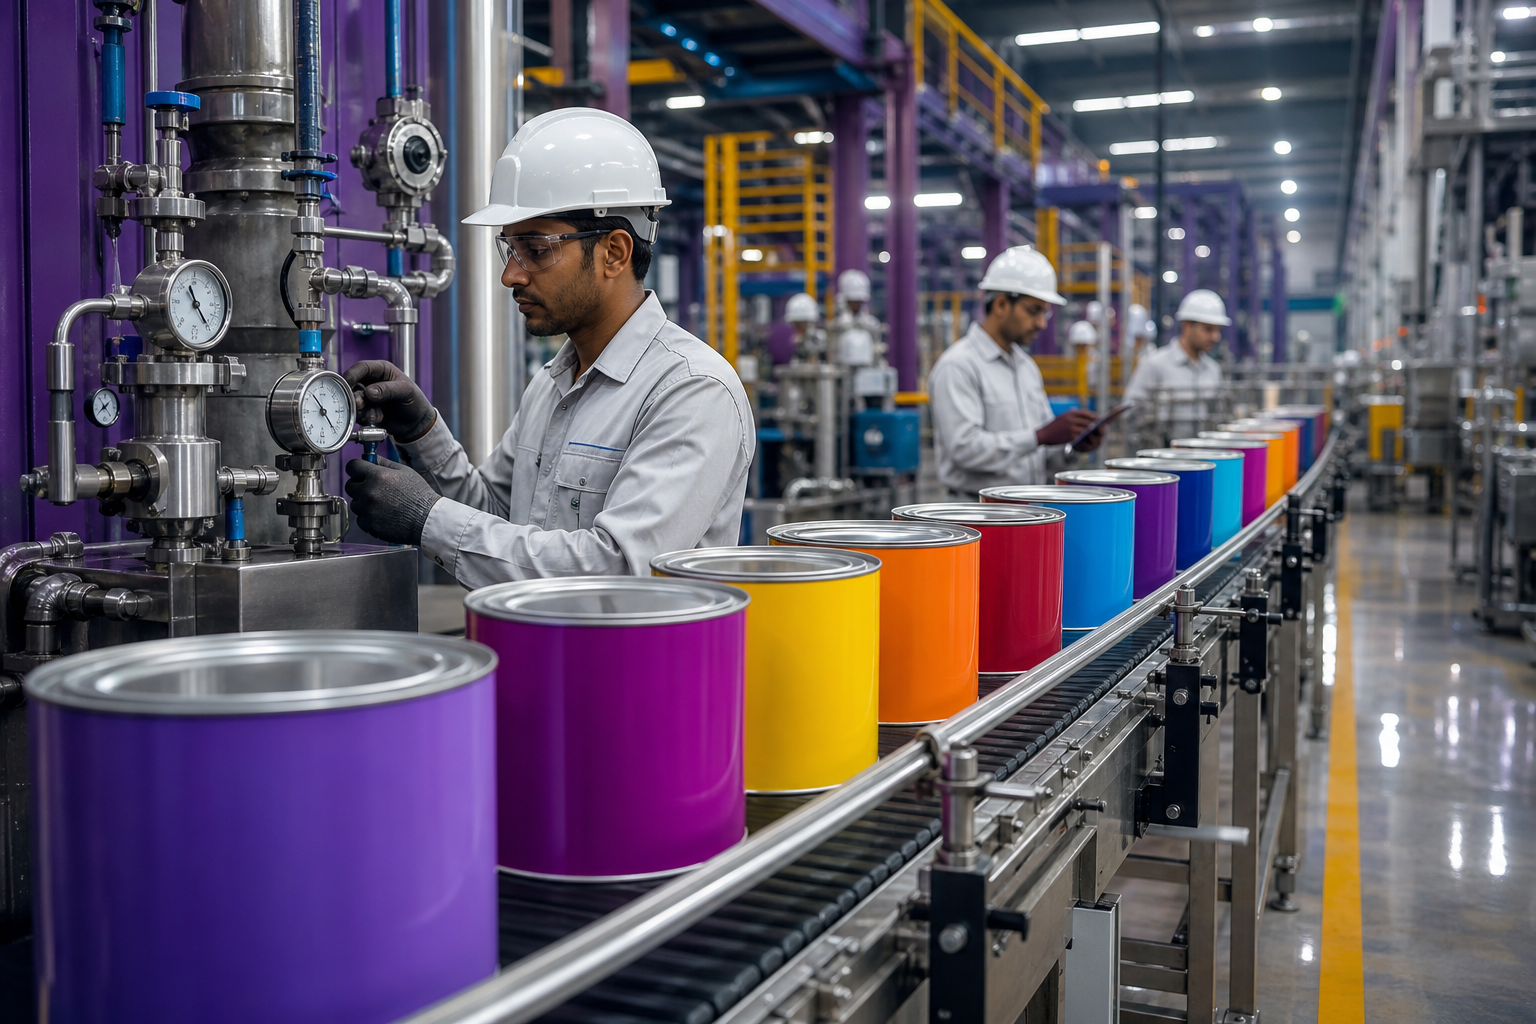
Situation. A paint business does not win merely by keeping mixers, filling lines, and packing equipment busy. It must produce the right colours, pack sizes, and SKUs fast enough for dealers, while avoiding rework, contamination, and stockouts. In such a setting, a simple “machine utilization” target can push the plant to run long batches that look efficient but hurt responsiveness.
The move. An OEE lens would separate losses by line and product family: downtime during changeovers, slow filling speeds for difficult packs, and quality losses from shade mismatch, leakage, or rework. The improvement agenda would not be “raise OEE everywhere.” It would be to improve OEE at the constraint while protecting mix flexibility and customer service. Supporting levers would include better preventive maintenance, faster changeover routines, stronger in-process quality checks, and tighter coordination with planning.
Lesson. The primary driver of better OEE is loss visibility at the constraint. The supporting drivers are maintenance discipline, changeover capability, quality control, and planning alignment. This is why OEE must be read with flow and customer-service metrics, not as an isolated factory trophy.
How AI Changes Overall Equipment Effectiveness
AI is making OEE more real-time, more predictive, and less dependent on manual logbooks.
A practical student workflow: load this lesson, a company annual report, and a simple production dataset into NotebookLM. Ask it to generate five likely interview questions on OEE, identify which component each question tests, and suggest what extra data you would request as an operations manager.
AI also connects OEE with adjacent decisions. For example, if low availability is caused by missing materials rather than machine breakdown, the fix belongs partly in replenishment logic; that is where using AI for inventory optimisation and replenishment becomes relevant. If the issue is starvation and overproduction between stations, revisit Kanban and pull-based replenishment.
Interview Relevance
“A plant manager says the OEE of a packaging line is 62%. How would you interpret this, and what actions would you recommend?”
If you are given only OEE, say: “I would not prescribe a fix until I see the three components and the loss Pareto.” That one sentence signals managerial maturity.
Common Mistake
The mistake is treating OEE as a single score to maximise everywhere. It costs candidates because it leads to generic answers like “reduce downtime” without diagnosing the real loss. The fix: split OEE into availability, performance, and quality, then improve the largest loss at the bottleneck.