
The Seven Wastes and How to Spot Them on Site
The same shop floor can look completely different before and after you learn to see waste. First you notice busy people, stacked bins and machines running; then you notice parts travelling twice, operators searching for tools, WIP ageing between stations and rework quietly eating capacity.
- Lean waste is any activity that consumes resources without creating customer value.
- The seven classic wastes are remembered as TIMWOOD: Transport, Inventory, Motion, Waiting, Overproduction, Overprocessing and Defects.
- On site, do not ask “Is everyone working?” Ask “Is the product or customer moving closer to value?”
- Overproduction is often the worst waste because it hides the others inside excess stock.
- Use observation tools: waste walk, spaghetti diagram, WIP count, first-pass yield, cycle time and value-added ratio.
- Good Lean diagnosis separates symptom from root cause: waiting may be caused by poor line balance, changeover delay or missing material.
- The strongest interview answer links each waste to a business impact: cost, lead time, quality, cash or safety.
Big Picture: Waste Is Busy Work That the Customer Would Not Pay For
Lean thinking begins with a brutal question: if the customer could watch this step, would they willingly pay for it? If the answer is no, the activity is either waste or a necessary non-value-added activity that must be simplified.
Core Explanation: The Seven Wastes and Their Site Signals
The seven wastes are not a theory to memorise; they are a lens for walking a factory, warehouse, branch, hospital, kitchen or service desk. The trick is to watch the flow of work, not the apparent effort of people.
The mnemonic TIMWOOD keeps the list interview-ready.
Overproduction deserves special attention. It is called the most dangerous waste in many Lean systems because once you make too much, you need transport to move it, inventory to store it, motion to manage it, waiting because queues grow, overprocessing to track it and defects hidden inside it.
How to Spot the Seven Wastes During a Site Walk
A strong site walk is not a casual tour. It is a structured observation of how material, information and people move through the process. If you already understand what Lean actually is and where it came from, this is the practical skill that turns Lean vocabulary into diagnosis.
Waste-Spotting Metrics You Can Calculate Fast
Do not over-engineer measurement. For a first diagnosis, five simple measures are enough to prove where waste is hurting flow.
Worked example: Suppose one order spends 4 minutes being assembled, 2 minutes being inspected, 18 minutes waiting in a queue and 6 minutes moving between stations. If only assembly changes the product in a way the customer values, value-added time is 4 minutes and total lead time is 30 minutes. Value-added ratio = 4 ÷ 30 × 100 = 13.3%. The diagnosis is not “people are slow”; it is “most lead time is waiting and movement.”
The Waste Priority Matrix: What to Attack First
Not every waste should be attacked with the same urgency. Prioritise wastes that are frequent and expensive first; treat rare but severe wastes through risk controls; and do not spend senior management energy on low-impact irritants before the main flow constraint is fixed.
Definitions You Should Be Able to Say in One Breath
- Lean waste: Any activity that consumes resources but does not create customer value.
- Value-added activity: A step that transforms the product or service in a way the customer is willing to pay for.
- Necessary non-value-added activity: Required work, such as compliance or safety checks, that should be simplified but not blindly removed.
- Muda: The Japanese Lean term for waste, commonly taught with mura, unevenness, and muri, overburden, in the Toyota Production System.
Case Study: Aravind Eye Care System and Waste Removal in a Service Flow
Aravind Eye Care System shows how Lean waste thinking applies beyond factories: it designs patient flow so doctors spend more time on high-value clinical work and less time on avoidable waiting, motion and handoff confusion.
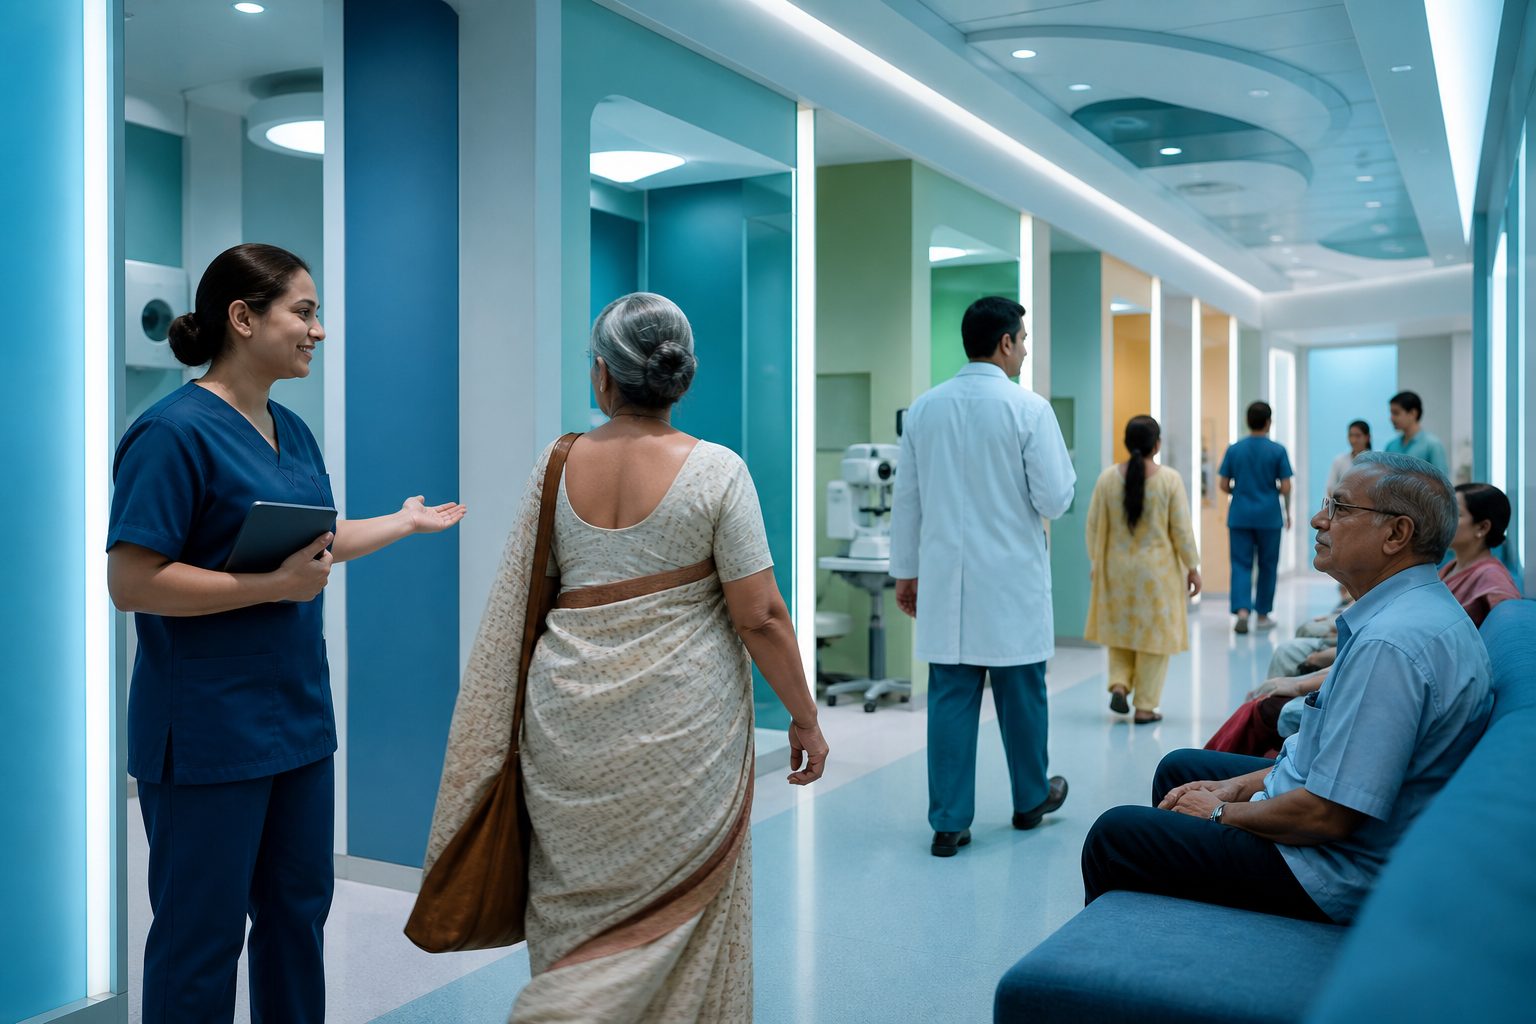
Situation: In a high-volume eye-care environment, the scarce resource is expert clinical time. If surgeons or specialists spend time waiting for patients, searching for information, repeating basic preparation or handling avoidable handoffs, the system loses capacity even when everyone appears busy.
The move: Aravind built a repeatable flow around task separation, standard routines and prepared handoffs. Basic screening, patient preparation, clinical examination, surgery support and recovery are organised so specialised doctors focus on the work only they can do. The primary driver is flow design around the bottleneck skill. Supporting drivers include standardised work, trained support staff, visual patient movement, disciplined scheduling and continuous improvement of handoffs.
The lesson: This is the seven-wastes lens in a service operation. Waiting falls when patients and information are ready. Motion falls when tools, records and support are arranged around the clinician. Overprocessing falls when each step has a clear purpose. Defects fall when handoffs are standardised and checked.
So what: The case proves that Lean waste is not about making people work harder. It is about designing work so scarce capability is used on value creation, while avoidable movement, waiting, rework and confusion are removed.
How AI Changes the Seven Wastes and How to Spot Them
AI does not replace the waste walk; it makes weak signals easier to see. In 2026, the biggest shift is that teams can combine human observation with digital traces from cameras, scanners, ERP systems, warehouse systems and service tickets.
- Computer vision for motion and waiting: Video analytics can flag repeated walking, queue build-up, blocked aisles or idle machines. The caution is privacy and context: AI may detect movement, but only a process owner can decide whether that movement is waste or necessary work.
- Process mining for information waste: Event logs from ERP, CRM or ticketing systems can reveal rework loops, approval delays, duplicate entries and ageing cases that are invisible during a short physical visit.
- AI-assisted root cause clustering: Defect notes, maintenance comments and customer complaints can be grouped by pattern so teams see recurring causes instead of treating every issue as isolated.
Before an operations interview, load your site-walk notes, a simple process map and any public company description into ChatGPT or NotebookLM. Ask: “Classify each observation under TIMWOOD, suggest one metric for each, and separate symptoms from possible root causes.” Then manually validate the answer - especially safety, labour and quality assumptions.
If your discussion moves from waste spotting to replenishment signals, revise Kanban and pull-based replenishment; if it moves to stabilising the workplace, revise standard work, visual management and workplace organisation.
Interview Relevance
“You are walking through a manufacturing plant or warehouse and see piles of WIP, operators waiting near machines and material being moved back and forth. How would you diagnose Lean waste?”
Use this sentence in interviews: “I would not begin by blaming labour productivity; I would follow one unit of work and identify where flow stops, reverses, piles up or gets corrected.”
Common Mistake
The mistake: Candidates list TIMWOOD correctly but treat waste as a people problem - “operators are idle,” “workers are walking,” “staff are slow.” This costs marks because Lean diagnoses system design, not individual busyness. One-line fix: say, “I will observe the flow first, classify the waste, measure its impact and then look for the process cause.”