
Layout Design: Process, Product & Cellular
Walk into a job shop and you may see parts travelling like tourists - cutting in one corner, drilling in another, inspection somewhere else, with trolleys waiting in aisles. Walk into a well-designed assembly line and the same work feels almost inevitable: one step hands off to the next, movement is short, and delay becomes visible.
- Layout design decides where people, machines, materials and information sit so work flows with minimum waste.
- Process layout groups similar resources together - flexible for high variety, but often creates longer travel and waiting.
- Product layout arranges resources in the exact sequence of operations - efficient for high volume, but less flexible.
- Cellular layout groups machines and people around a product family - a middle path between flexibility and flow.
- The core decision is the volume-variety trade-off: high variety pulls you toward process layout; high volume pulls you toward product layout.
- Judge a layout using travel distance, throughput time, WIP, space use, changeover burden and line/cell balance.
- Interview answer rule: never name a layout first. Diagnose product variety, volume, routing similarity, demand stability and constraints first.
Big Picture: Layout Is the Physical Strategy of a Process
A layout is not a drawing exercise. It is an operations strategy decision made visible on the shop floor. The same machines can produce very different cost, speed and service outcomes depending on where they are placed and how work moves between them.
Use this mental map: variety creates routing complexity; volume rewards repetition. Layout design is the attempt to balance both without hiding waste.
Core Explanation: The Three Layouts You Must Be Able to Compare
Layout design is the arrangement of facilities, resources and work areas to enable safe, smooth and economical flow. In interviews, the topic is usually tested through a messy process: a hospital, warehouse, machine shop, quick-service kitchen, bank branch or assembly operation.
1. Process Layout - Flexibility First
A process layout groups similar activities or equipment together: all drilling machines in one area, all inspection in another, all billing counters in another. It is common when products follow different routes.
Its strength is flexibility. Its weakness is movement. Because each order may need a different path, material handling, queues and scheduling complexity rise. This is why a process layout often needs strong dispatching rules, visible WIP control and careful capacity management.
2. Product Layout - Flow First
A product layout arranges resources in the sequence in which a product or service is made. Think of automobile final assembly, packaged food filling lines or a cafeteria tray line.
Its strength is speed and unit cost. Its weakness is rigidity. If demand shifts, product mix changes or one station fails, the whole line can be affected. Product layout works best when volume is high, demand is stable and tasks can be balanced across workstations. If that last phrase feels important, revise Line Balancing and Workstation Design after this lesson.
3. Cellular Layout - Flow Around Families
A cellular layout groups different machines and people into a mini-system dedicated to a family of similar products. Instead of sending a part across the factory, the part moves inside a compact cell where most or all required operations happen nearby.
The logic comes from group technology: identify product families with similar processing needs, then build a cell around that family. It is especially powerful when products are not identical but have enough routing similarity to justify flow.
When to Use Which Layout
The most interview-safe way to choose a layout is to diagnose five conditions: volume, variety, routing similarity, demand stability and the cost of movement. Do not jump straight to the answer.
Notice the hidden trade-off: a process layout usually maximises equipment flexibility, while a product layout maximises flow efficiency. Cellular layout tries to capture flow without forcing every product into one rigid line.
The Layout Design Process: A Practical Five-Step Method
If an interviewer gives you a factory or service redesign problem, use this sequence. It sounds structured, but it also mirrors how real operations teams approach layout work.
For the first step, do not rely only on verbal descriptions. A simple process map or spaghetti flow will reveal waste faster than a meeting. If you need to strengthen that skill, revise Process Mapping and Value Stream Mapping.
Metrics: How to Judge Whether a Layout Is Better
A layout is better only if it improves measurable flow without creating a new constraint. These are the six measures to quote confidently.
For WIP and flow time, the mathematical bridge is Little's Law: WIP equals throughput rate multiplied by flow time. If a layout reduces waiting and movement, it should normally reduce WIP or lead time; revise Little's Law and Reading a Process Mathematically if you want the numerical base.
Worked Example: Choosing a Layout with Simple Numbers
Suppose a workshop makes three part families. Each part currently travels between cutting, drilling, grinding and inspection departments.
The proposed cellular layout reduces daily travel from 12,000 metres to 3,200 metres in this illustration. That is not automatically approval. You would still check cell utilisation, operator skills, changeover time, equipment duplication and whether any new bottleneck appears. If one resource now limits the cell, connect this analysis to Finding the Bottleneck and the Theory of Constraints.
Definitions You Can Say in One Breath
- Layout design: Arrangement of resources and work areas to support safe, economical and smooth flow.
- Process layout: A layout that groups similar activities or equipment together for flexible routing.
- Product layout: A layout that places resources in the sequence required to make one product or service.
- Cellular layout: A layout that groups resources into cells serving families with similar processing needs.
- Group technology: A method of classifying parts or products into families based on design or processing similarity.
Case Study: Lenskart and the Layout Logic of High-Variety Eyewear
Lenskart is a useful Indian example because prescription eyewear combines huge variety with repeated processing steps, making layout choice strategically important.
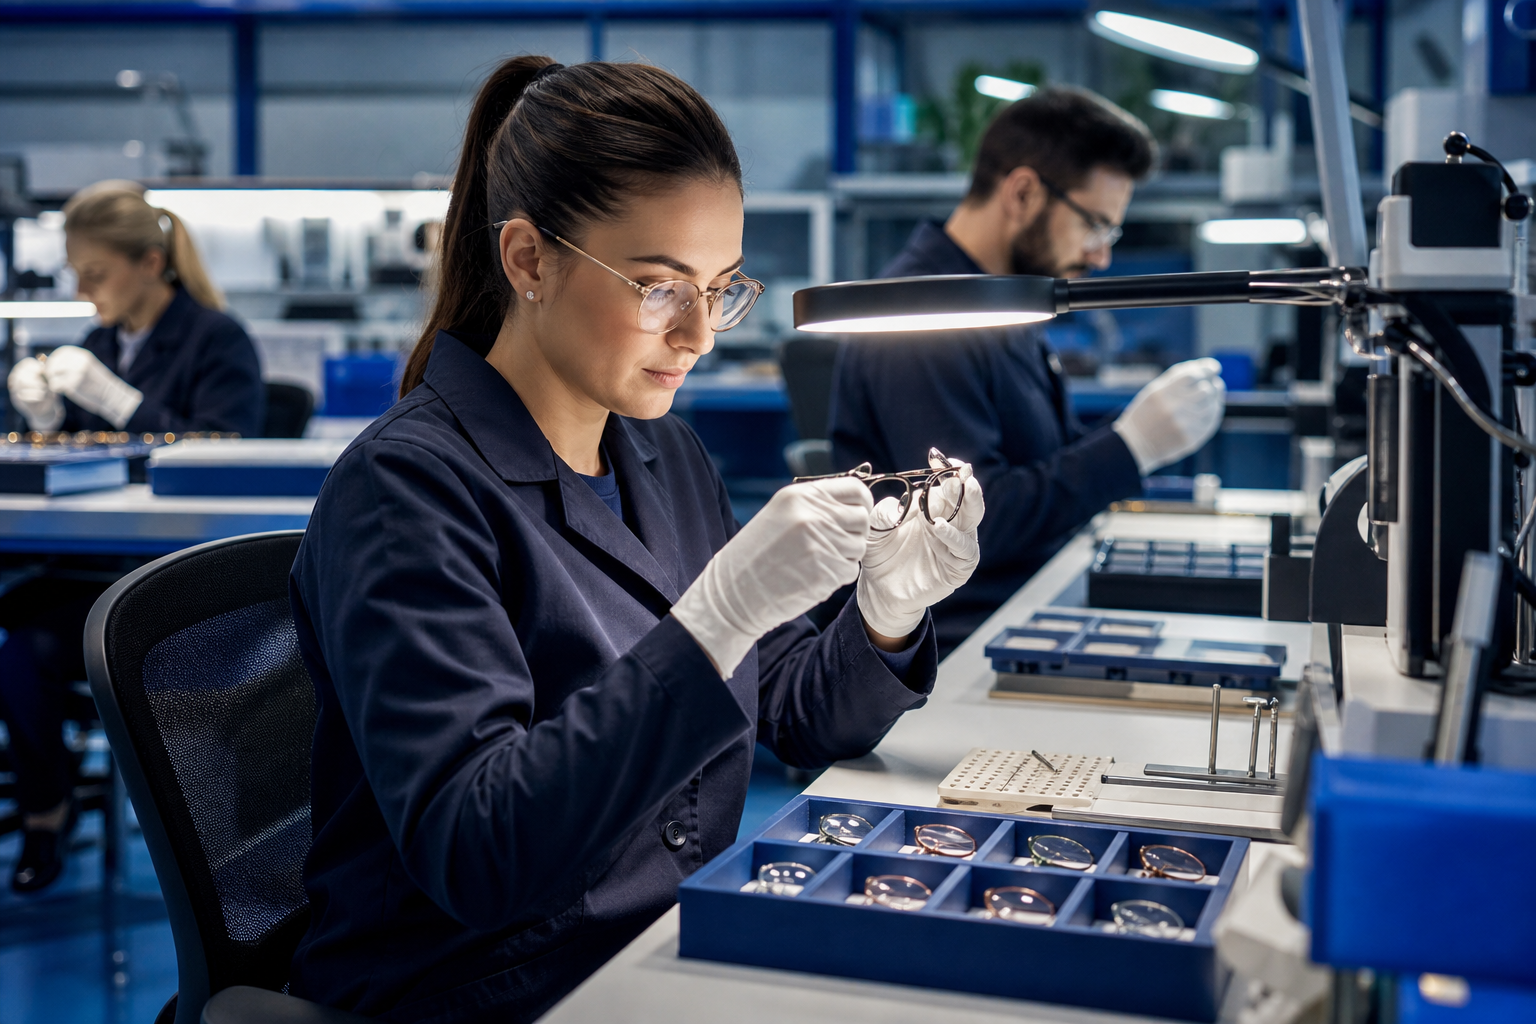
Prescription eyewear is operationally tricky. Two customers may buy similar frames, but their lens powers, coatings, fitting needs and delivery promises can differ. If every order is treated like a completely unique job, the operation becomes a slow process layout with too much travel and waiting. If every order is forced into one rigid line, variety can break the flow.
The smarter layout logic is hybrid. Keep specialised capabilities where expertise or equipment sharing matters, but create flow for repeatable families: frame picking, lens preparation, fitting, quality check and dispatch. In a business like Lenskart, the primary driver is not simply automation; it is matching a high-variety product to a repeatable fulfilment flow. Supporting drivers include digital order visibility, standardised work, quality checks, inventory positioning and trained teams that can handle prescription variation without losing speed.
The interview takeaway: do not label a company as purely process, product or cellular. Real operations often use a dominant layout logic plus supporting layout pockets. That is how you sound like an operations thinker rather than someone reciting definitions.
How AI Changes Layout Design: Process, Product & Cellular
AI does not remove the need for layout judgment; it improves the quality and speed of layout testing. Three changes matter in 2026.
The practical student workflow: upload a current-state process map, SKU routing table and manager notes into ChatGPT or Claude, then ask it to propose three layout alternatives, list assumptions, and design a comparison table using travel distance, WIP, throughput time and bottleneck risk. For a deeper operations simulation mindset, use Using AI and Simulation to Test a Process Design as the natural next step.
Interview Relevance
A plant makes many low-volume customised parts. Management wants faster delivery and lower WIP. Would you recommend a process layout, product layout or cellular layout?
Use the phrase: “I would not choose a layout by name; I would choose the dominant flow logic after checking volume-variety and routing similarity.” It immediately upgrades your answer.
Common Mistake
The biggest mistake is saying “product layout is best because it is efficient.” It costs candidates because efficiency without variety-fit creates stoppages, rework, queues and poor responsiveness. One-line fix: first diagnose volume, variety and routing similarity, then choose the layout.