
Manufacturing Footprint and Plant Loading Decisions
A factory can be profitable on paper and still be the wrong factory to load. The surprise is that the cheapest plant is not always the best plant - once freight, duties, lead time, risk, quality capability and capacity cushion enter the decision, the answer can flip.
- Manufacturing footprint is the network of plants, contract manufacturers and capacity locations that serve demand.
- Plant loading decides which products, volumes and markets each plant should handle within capacity and capability limits.
- The best answer is rarely "load the lowest-cost plant"; use landed cost, service level, flexibility and risk together.
- Start with demand by region and product, then check plant capability, capacity, total cost, risk and tax or regulatory constraints.
- Use metrics like utilisation, capacity cushion, OEE, landed cost per unit, OTIF and changeover loss.
- A good footprint balances efficiency today with optionality tomorrow - especially when demand is volatile or regulations shift.
Big Picture
Think of footprint decisions as the "where should we make?" question and plant loading as the "how much of what should each site make?" question. Footprint is structural and slower to change; loading is more tactical but still has strategic consequences.
Core Explanation
The central trade-off is simple: a highly concentrated footprint can give scale economies, but a distributed footprint can improve responsiveness and reduce disruption risk. The right answer depends on product economics, demand volatility, customer service expectations and the regulatory environment.
Manufacturing footprint decisions usually include plant location, plant role, capacity size, make-versus-buy boundaries, supplier ecosystem and regional market allocation. If ownership itself is in question, revise make versus buy and outsourcing economics before attempting a footprint case.
Plant loading decisions allocate specific SKUs, product families or customer volumes across the available network. Loading must respect both hard constraints such as installed capacity, tooling and certifications, and soft constraints such as learning curve, supplier maturity and customer proximity.
The Five-Step Framework for Plant Loading
This framework prevents the classic half-answer: "Plant A has lower cost, so put everything there." That answer ignores whether Plant A can actually absorb the volume without hurting service, quality or resilience.
Key Metrics to Track
In interviews, metrics make your answer operational. Use them to show that loading is not a preference - it is a measurable allocation problem.
A Small Worked Example
Suppose a company has two plants and two demand regions. The North plant has lower conversion cost, but the South plant is closer to the East market.
Demand is 20,000 units in West and 30,000 units in East. Landed cost is:
- North to West = ₹900 + ₹80 = ₹980
- North to East = ₹900 + ₹140 = ₹1,040
- South to West = ₹940 + ₹160 = ₹1,100
- South to East = ₹940 + ₹70 = ₹1,010
The best simple loading plan is: North serves all West demand of 20,000 units, North sends 5,000 units to East, and South serves the remaining 25,000 East units.
Total cost = 20,000 × ₹980 + 5,000 × ₹1,040 + 25,000 × ₹1,010 = ₹50.05 million. The lesson: the lower-cost plant should be loaded first only where its full landed cost and capacity position justify it.
Definitions
- Manufacturing footprint: The network of owned plants, outsourced sites and capacity locations used to manufacture and serve markets.
- Plant loading: The allocation of products, volumes and customer demand across plants within cost, capacity and capability constraints.
- Plant role: The strategic purpose of a site, such as scale production, regional responsiveness, export supply or specialised manufacturing.
- Capacity cushion: The spare capacity kept above expected demand to absorb variability, downtime and demand spikes.
- Landed cost: The full cost of making and delivering a unit to the customer, including logistics, duties, inventory and quality costs.
Case Study - Dixon Technologies: Loading a Multi-Category EMS Footprint
Dixon Technologies shows why plant loading in electronics manufacturing is a portfolio decision across categories, customers, capabilities and supply ecosystems.
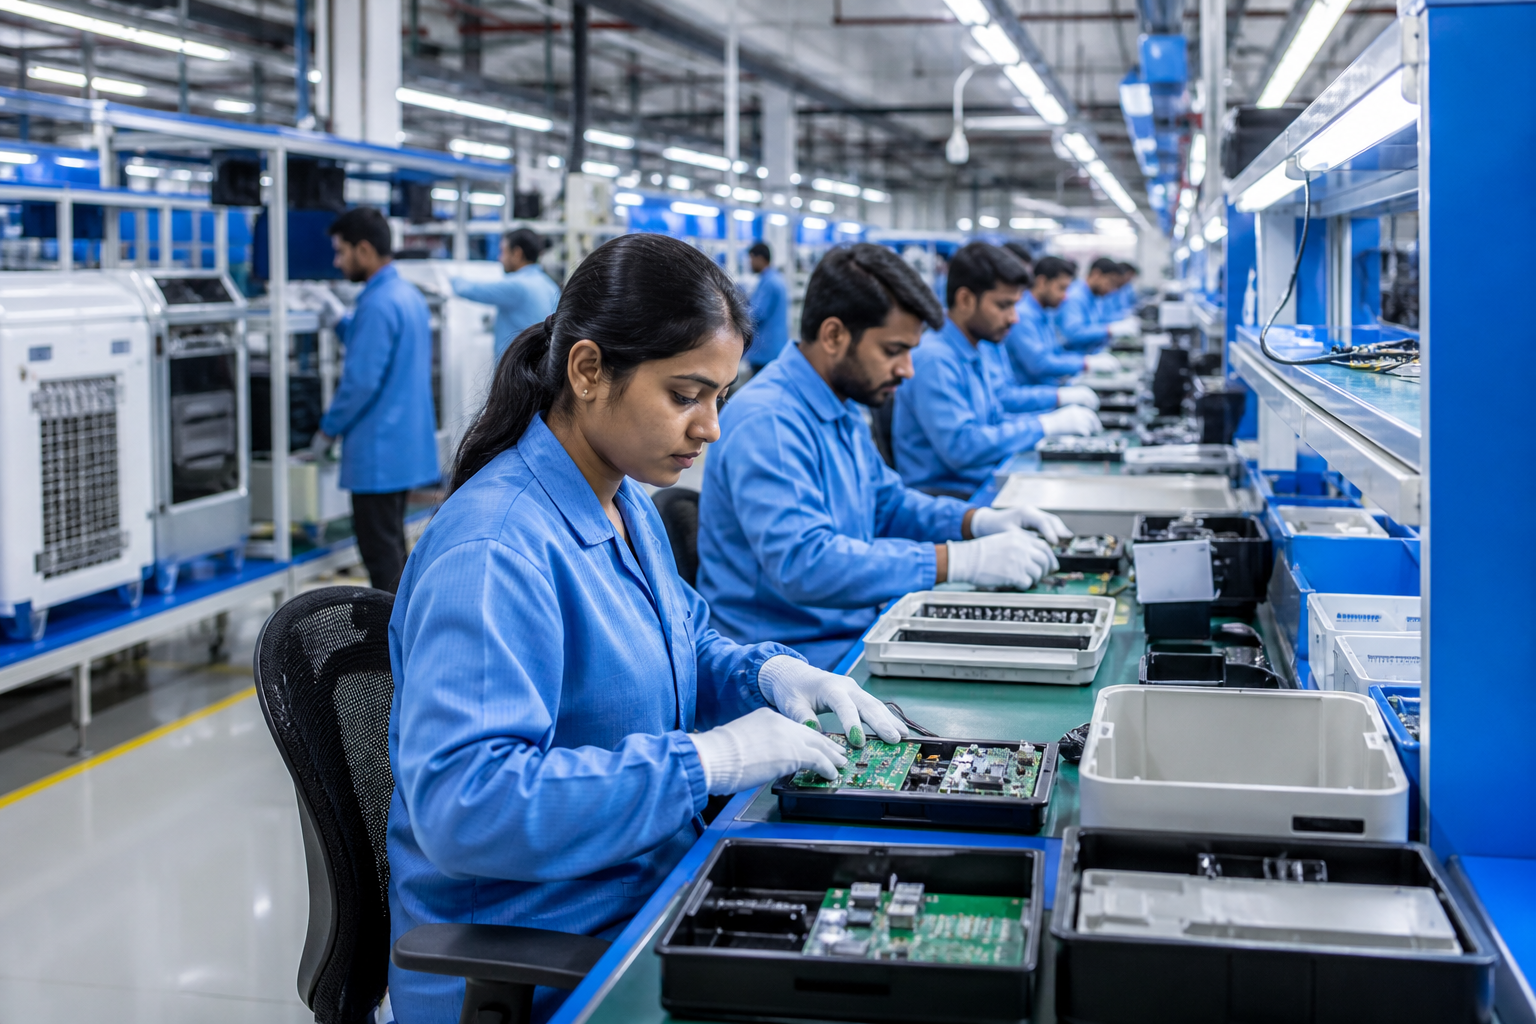
Dixon Technologies is a useful Indian example because electronics manufacturing services rarely have one clean product flow. A site may handle consumer electronics, lighting products, mobile devices, appliances or components, but each category has different tooling, labour content, quality requirements, supplier dependencies and customer delivery windows.
Situation: An EMS manufacturer serving multiple brands cannot simply spread volume evenly across plants. A television line, mobile assembly line and appliance line may all need capacity, but they do not consume the same bottleneck resources.
The move: The practical footprint logic is to create plant roles by category and customer requirement: high-volume, stable products go to more standardised scale lines; more variable or customer-specific work needs flexible capacity and faster changeover capability. This only works when supported by supplier proximity, trained labour, quality systems and customer coordination.
The lesson: The primary driver is category-specific manufacturing economics. Supporting drivers include customer commitments, supplier ecosystem, labour skill, regulatory eligibility, working-capital needs and quality risk. A weak answer says "Dixon should load the cheapest plant." A strong answer asks which plant is best suited for that product family at the required service level.
How AI Changes Manufacturing Footprint and Plant Loading Decisions
AI is making footprint and loading decisions more dynamic, but it does not remove managerial judgment. It improves the quality of scenarios, alerts and trade-off analysis.
- Scenario simulation: AI models can test demand surges, supplier disruption, freight delays and capacity bottlenecks faster than manual spreadsheets. The manager still defines the scenarios that matter.
- Demand-aware loading: ML-based forecasts can update plant loading plans by SKU, region and season. This connects naturally with AI-based inventory optimisation and replenishment, because production allocation and inventory policy must agree.
- Bottleneck detection: Computer vision, machine data and production logs can identify chronic downtime, quality losses and changeover delays before they become network-level constraints. If the problem is inside the line, revise line balancing and workstation design before recommending a new plant.
Use NotebookLM or ChatGPT with a company annual report and ask: "List the company's manufacturing locations, product categories, capacity risks, supplier dependencies and possible plant-loading trade-offs." Then convert the output into the five-step framework above.
Interview Relevance
"A consumer durable company has plants in North and South India. Demand is growing in the West, freight costs are rising, and one plant is underutilised. How would you decide the manufacturing footprint and plant loading plan?"
Always separate plant location from plant loading. A company may keep the same footprint but change loading to improve service, utilisation or resilience.
Common Mistake
The most common mistake is choosing the lowest conversion-cost plant and stopping there. It costs candidates because interviewers expect a total network view, not a factory-cost answer. One-line fix: compare options on landed cost, capacity, service, flexibility and risk before recommending the load plan.